Thermal Oil Heater Design by PT Indira Mitra Boiler
A Thermal Oil Heater is an industrial heating system that uses heat-transfer oil as the circulating medium. The system can generally operate at temperatures up to approximately 300–320°C, depending on the thermal-fluid specification, heater design, and operating conditions.
Unlike a steam boiler, a thermal oil heater can produce high process temperatures without requiring high operating pressure. For comparison, a steam system may require considerable pressure to achieve temperatures approaching 285°C. A thermal oil system normally operates only with the pressure generated by its circulation pump and the resistance of the piping network.
This characteristic makes a Thermal Oil Heater system suitable for industrial processes that require stable, precise, and continuous heating at high temperatures.
PT Indira Mitra Boiler designs and supplies thermal oil heater systems for various industrial applications, including reactors, dryers, tanks, heat exchangers, presses, asphalt plants, chemical processes, food processing, and other heating equipment.
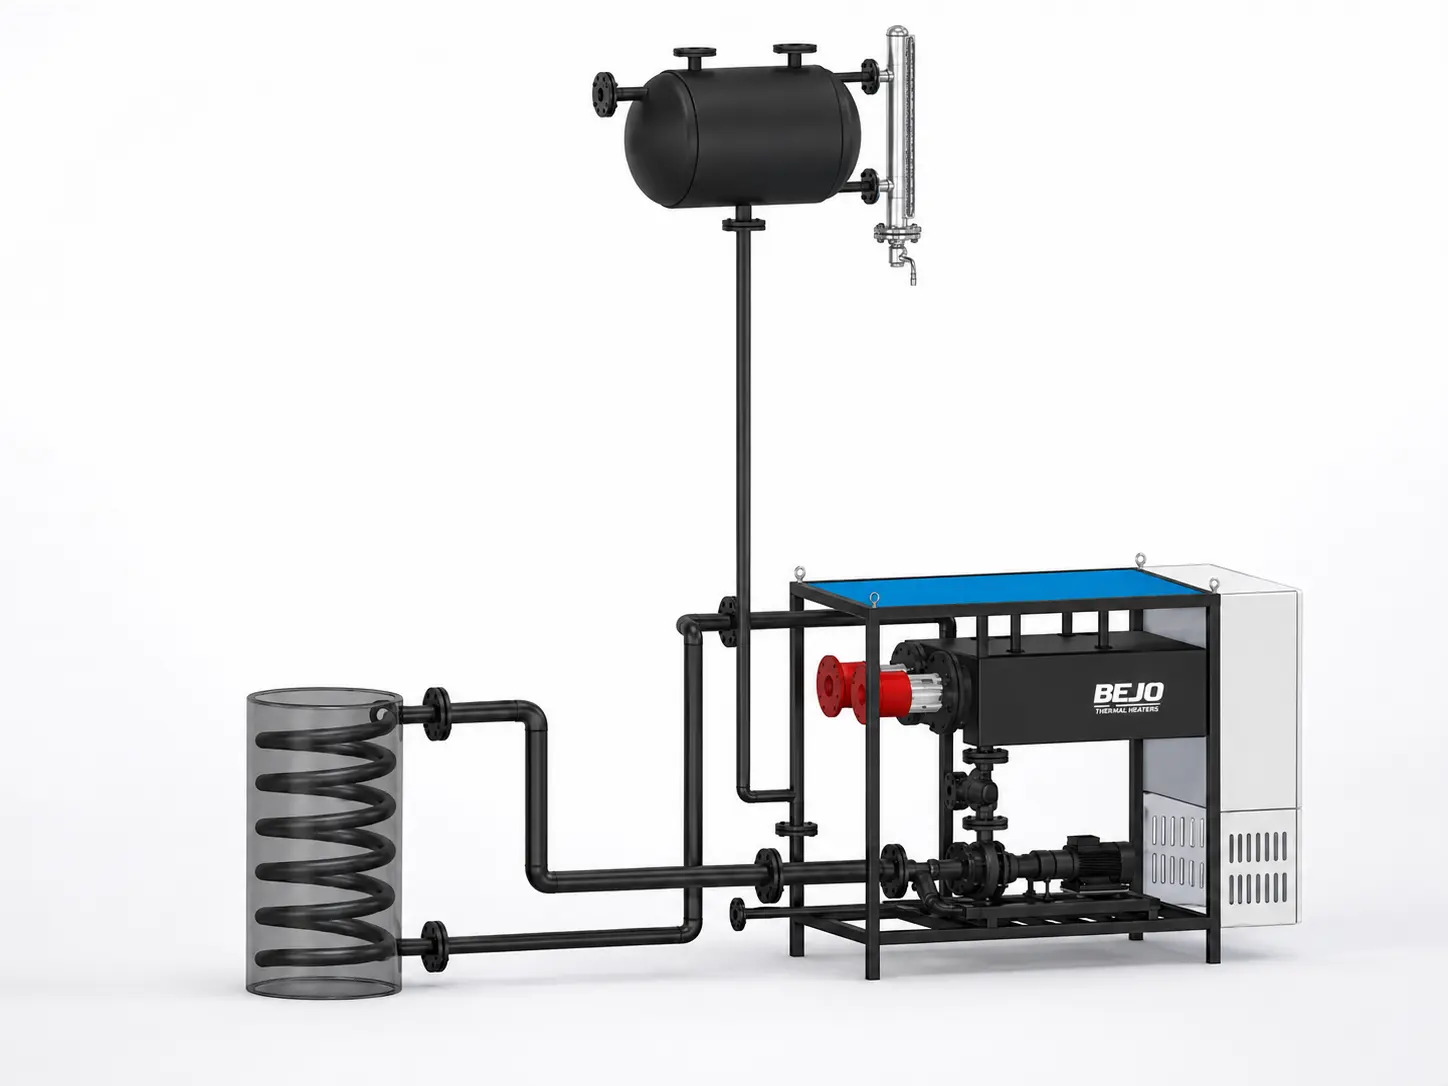
Understanding a Thermal Oil Heater
A thermal oil heater is a heat-generating unit in which thermal fluid circulates through a heating coil. A burner supplies combustion heat to the coil, and the heated fluid transports that thermal energy to the production equipment.
After releasing heat to the process, the thermal oil returns to the heater and is reheated. This creates a closed-loop circulation system.
The main operating cycle is:
- The circulation pump moves thermal oil through the heater coil.
- The burner produces heat inside the combustion chamber.
- Radiant and convection heat is transferred to the oil inside the coil.
- Hot thermal oil flows toward the process equipment.
- The process absorbs the required heat.
- Cooler return oil flows back to the thermal oil heater.
- The heating and circulation cycle continues automatically.
Because the fluid remains in liquid form during normal operation, the system does not experience steam condensation, flash-steam losses, or boiler blowdown losses.
Advantages of a Thermal Oil Heater Compared with a Steam Boiler
Several operational and technical factors can make a thermal oil heater more suitable than a steam boiler for high-temperature process heating.
1. High Operating Temperature at Low Pressure
A thermal oil system can deliver high process temperatures without the high pressure normally required by steam.
The actual operating pressure is primarily generated by the circulation pump and piping resistance. However, all components must still be designed according to the system’s maximum pressure, temperature, thermal-fluid properties, and applicable engineering standards.
2. Precise Temperature Control
Thermal oil heaters can be equipped with automatic temperature controllers and modulating burners. This arrangement provides stable temperature control for processes that require consistent heating.
A temperature sensor installed in the thermal oil supply line sends a signal to the control system. The burner capacity is then adjusted according to the process heat demand.
3. No Boiler-Water Treatment
A thermal oil system does not use water as its primary heat-transfer medium. Therefore, it does not require conventional boiler-water treatment for scale, hardness, dissolved oxygen, and alkalinity control.
Nevertheless, the thermal fluid must be periodically tested to determine its viscosity, acidity, carbon residue, flash point, contamination level, and remaining service condition.
4. No Condensate or Blowdown Losses
A thermal oil system does not generate condensate and does not require routine boiler blowdown. This can reduce energy losses, water consumption, chemical consumption, and wastewater production.
5. Low Internal Corrosion Risk
When the correct thermal fluid is used and the system is properly designed, thermal oil generally does not create internal corrosion and mineral scale in the same way untreated boiler water can.
However, corrosion may still occur because of moisture contamination, oxidation, incorrect material selection, external environmental exposure, or poor system maintenance.
6. Low Maintenance Requirements
A properly operated thermal oil heater can require less routine treatment than a steam boiler. There is no regular boiler-water blowdown and no conventional water-scale cleaning.
Maintenance is still required for:
- Burner and combustion system
- Circulation pump and mechanical seal
- Thermal oil quality
- Heating coil
- Strainer
- Valves and flanges
- Expansion tank
- Safety interlocks
- Temperature and pressure instruments
- Electrical control panel
- Chimney and exhaust system
7. Fully Automatic Operation
Modern thermal oil heaters can operate automatically using temperature controllers, burner controllers, pressure switches, flow switches, level switches, alarms, and shutdown interlocks.
Although the operation is automatic, only trained and authorized personnel should operate or maintain the equipment.
Vertical and Horizontal Thermal Oil Heater Design
PT Indira Mitra Boiler can provide vertical or horizontal thermal oil heater designs, depending on site conditions, required capacity, combustion system, maintenance access, and process requirements.
Vertical Thermal Oil Heater
A vertical thermal oil heater can provide the following advantages:
- Smaller installation footprint
- Compact equipment arrangement
- Efficient use of limited plant space
- Integrated burner installation
- Easier placement in certain boiler-room layouts
- Suitable for small to large heating capacities
Horizontal Thermal Oil Heater
A horizontal thermal oil heater may be selected when:
- The available space is wider than it is high
- Overhead clearance is limited
- The customer requires horizontal maintenance access
- The existing production layout is better suited to a horizontal unit
- Transportation or site installation conditions require this configuration
The final orientation must be determined through engineering calculations and a review of the installation area.
Thermal Oil Heating-Coil Construction
The heating coil is one of the most important parts of a thermal oil heater. It absorbs combustion heat and transfers it to the circulating thermal oil.
The coil is commonly manufactured from seamless boiler tube selected according to:
- Design temperature
- Design pressure
- Thermal-fluid specification
- Required thermal capacity
- Oil circulation velocity
- Corrosion allowance
- Applicable material and fabrication standards
The coil may be arranged in concentric spirals to create radiant and convection heating surfaces.
Welded joints must be completed using qualified procedures and inspected according to the specified manufacturing standard. Appropriate testing may include visual inspection, penetrant testing, radiographic testing, ultrasonic testing, or pressure and leak testing.
The type of pressure-test medium and test pressure must follow the approved design code and manufacturer’s procedure. Pneumatic testing presents significant stored-energy risk and must only be performed under an approved safety procedure.
Three-Pass Thermal Oil Heater Design
In a three-pass thermal oil heater, combustion gas travels through three heating zones before entering the chimney.
The general heat-transfer sequence includes:
First Pass: Radiant Heating
The burner flame releases radiant heat inside the combustion chamber. The inner heating coil absorbs a large portion of this energy.
Second Pass: Convection Heating
After leaving the radiant chamber, the combustion gases pass through the space between the coil arrangements. Heat is transferred by convection to the thermal oil.
Third Pass: Final Heat Recovery
The remaining hot gas passes across another heating surface before flowing toward the exhaust connection and chimney.
An appropriately designed gas velocity can improve heat transfer and help reduce soot accumulation on the outer surface of the coil. However, it does not eliminate the need for routine inspection and cleaning, especially when firing diesel, heavy oil, waste oil, or other fuels that may produce deposits.
Counterflow Heat-Transfer Principle
The combustion-gas path can be arranged in the opposite direction to the thermal-oil flow. This counterflow configuration helps maintain an effective temperature difference between the gas and the thermal fluid.
Correct oil velocity inside the coil is essential. Insufficient flow may cause local overheating, thermal cracking, sludge formation, carbon deposits, and premature deterioration of the thermal oil.
For this reason, the burner must not operate without confirmed thermal-oil circulation.
Air Preheater for Improved Efficiency
Certain thermal oil heater systems can be equipped with an air preheater. This component recovers residual heat from the exhaust gas and uses it to preheat combustion air before it enters the burner.
Potential benefits include:
- Improved combustion efficiency
- Reduced fuel consumption
- More stable combustion
- Lower exhaust-gas energy losses
- Improved atomization performance for certain liquid fuels
The air preheater must be selected carefully. Excessive air temperature, fouling, corrosion, and increased exhaust-system resistance must be considered during engineering.
Main Components of a Thermal Oil Heater System
A complete industrial thermal oil heater system generally includes the following equipment.
1. Thermal Oil Heater Unit
The main heater consists of:
- Combustion chamber
- Radiant heating coil
- Convection heating coil
- Outer casing
- Thermal insulation
- Inspection and cleaning access
- Thermal-oil inlet and outlet
- Flue-gas outlet
- Burner mounting
- Temperature and pressure instruments
2. Fuel Burner
The burner produces the heat required by the system. Depending on the project, the burner may use:
- Natural gas
- CNG
- LPG
- Biogas
- Diesel or light oil
- Heavy fuel oil
- Waste oil, subject to suitable preparation
- Dual-fuel combinations
Burner capacity must be calculated from the process heat load, thermal losses, start-up time, operating temperature, fuel characteristics, and heater efficiency.
3. Thermal-Oil Circulation Pump
The circulation pump moves thermal oil continuously through the heater coil and process equipment.
Pump selection must consider:
- Required flow rate
- Total dynamic head
- Thermal-fluid viscosity
- Operating temperature
- Pump material
- Mechanical-seal design
- Net positive suction head
- System pressure losses
- Standby-pump requirements
For critical processes, installing two pumps in a one-duty and one-standby configuration is recommended.
4. Expansion Tank
Thermal oil expands as its temperature rises. The expansion tank accommodates this increase in fluid volume and helps maintain stable system operation.
Its design and position must allow thermal expansion without creating excessive system pressure. The tank may also be equipped with nitrogen blanketing to reduce oxidation at elevated temperatures.
5. Thermal-Oil Collecting Tank
The collecting or drain tank stores thermal oil during maintenance, emergency draining, or system servicing.
The tank should have adequate capacity for the volume that may need to be drained safely from the heater and piping system.
6. Valves
The system can include:
- Isolation valves
- Drain valves
- Vent valves
- Bypass valves
- Control valves
- Non-return valves
- Emergency drain valves
Valve materials and pressure-temperature ratings must be suitable for hot thermal oil.
7. Strainer
A strainer protects the circulation pump and heating coil from welding debris, scale, sludge, carbon particles, and foreign material.
The pressure difference across the strainer must be monitored. A high differential pressure may indicate blockage and reduced thermal-oil flow.
8. Differential Pressure or Flow-Safety Instrument
A differential pressure switch, flow switch, or flow transmitter confirms that thermal oil is circulating through the coil.
If the flow falls below the safe limit, the safety system must stop the burner while maintaining the appropriate pump and shutdown sequence.
9. Control Panel
The thermal oil heater control panel may include:
- Main circuit breaker
- Burner controller
- Temperature controller
- High-temperature limiter
- Circulation-pump controls
- Pump overload protection
- Expansion-tank level alarm
- Differential-pressure interlock
- Flame-failure alarm
- Emergency stop
- Audible and visual alarms
- PLC and HMI, where required
- Automatic duty and standby pump sequencing
Selection of Thermal Oil Fluid
The thermal fluid must be selected according to the heater’s operating temperature and process requirements.
An ideal heat-transfer oil should have:
- High boiling point
- Good thermal stability
- Low pour point
- Good heat-transfer characteristics
- Suitable viscosity
- Resistance to oxidation
- Low vapor pressure
- Compatibility with seals and system materials
- Acceptable health and environmental properties
Thermal-fluid properties vary between products. The following values are only illustrative and must not replace the manufacturer’s technical data sheet:
- Density at approximately 200°C: around 760 kg/m³
- Specific heat: around 2.4 kJ/kg·K
- Flash point: around 180°C
- Autoignition temperature: around 370°C
- Initial boiling range: approximately 330°C
- Pour point: approximately −18°C
- Thermal-expansion coefficient: approximately 0.00076/°C
The maximum bulk-oil temperature and maximum film temperature specified by the oil manufacturer must never be exceeded.
Service Life of Thermal Oil
In a correctly designed and maintained system, thermal oil may remain usable for several years. However, a fixed service life cannot be guaranteed because fluid deterioration depends on:
- Operating temperature
- Film temperature at the coil wall
- Oxygen exposure
- Water contamination
- Fuel and combustion conditions
- Start-up and shutdown frequency
- System cleanliness
- Pump performance
- Presence of local overheating
- Mixing with incompatible fluids
Thermal-oil samples should be tested periodically. The oil should not be replaced solely according to age; its actual laboratory condition should be evaluated.
Thermal-Oil Heater Safety Warning
A thermal oil heater can cause fire, explosion, serious injury, equipment damage, and production losses when designed, operated, or maintained incorrectly.
The system must be operated according to:
- The manufacturer’s operating manual
- Approved start-up and shutdown procedures
- Applicable regulations and engineering standards
- Routine inspection schedules
- Emergency-response procedures
- Lockout and tagout requirements
Operators must receive appropriate training before operating the equipment.
Flue-Gas Temperature Limiter
A flue-gas temperature limiter detects an abnormal increase in exhaust-gas temperature.
An excessive flue-gas temperature may indicate:
- Soot deposits on the heating coil
- Reduced thermal-oil circulation
- Excessive burner capacity
- Incorrect combustion settings
- Coil leakage
- Poor heat transfer
- Abnormally high return-oil temperature
- Instrument failure
A thermal-oil leak into the combustion chamber is particularly dangerous. The leaking oil may ignite, produce heavy soot, intensify the fire, and cause an uncontrolled temperature rise.
When the exhaust temperature reaches the high-high limit, the system should initiate an alarm and burner shutdown. Restarting must be prevented until the cause has been inspected and the system is declared safe.
The alarm and trip values must be determined from the heater design, normal operating data, thermal-fluid limits, fuel type, and manufacturer’s recommendations.
Flame Detector
The flame detector confirms whether a stable burner flame exists.
If ignition fails or the flame disappears during operation, the burner-management system must close the fuel safety valves and stop the fuel supply. This prevents unburned gas or liquid fuel from accumulating inside the combustion chamber.
The flame-safeguard system should control:
- Pre-purge
- Ignition trial
- Pilot-flame verification
- Main-flame verification
- Fuel-valve operation
- Flame-failure shutdown
- Lockout and reset
Testing must follow the burner manufacturer’s approved procedure. Operators should not remove, bypass, cover, or manipulate a live flame sensor unless the procedure specifically requires it and the equipment has been placed in a safe test condition.
Every test and result should be recorded in the operating log.
Thermal-Oil Flow Limiter
A thermal-oil flow limiter protects the heating coil from operating with insufficient circulation.
Low flow can be caused by:
- Circulation-pump failure
- Closed or incorrectly positioned valve
- Blocked strainer
- Sludge or carbon deposits
- Pipe blockage
- Mechanical-seal or coupling failure
- Low oil level
- Excessive oil viscosity during cold start
- Electrical motor failure
The protection device may use:
- Differential pressure switch
- Flow switch
- Flow transmitter
- Pressure transmitter
- Pressure gauge with electrical contacts
A direct flow measurement is generally more reliable than relying only on pressure. The selected instrument should match the system design and required safety integrity.
If the thermal-oil flow falls below the safe limit, the burner must shut down automatically.
Expansion-Tank Low-Level Protection
The expansion tank should be equipped with a suitable level indicator and low-level switch.
A low oil level can indicate leakage at:
- Heating coil
- Circulation-pump seal
- Valve packing
- Flanged connection
- Process equipment
- Heat exchanger
- Pipe joint
- Drain connection
When the oil level reaches the minimum safe limit, the system should activate an alarm and shut down the burner according to the approved safety sequence.
A leak inside the furnace is especially dangerous because thermal oil may ignite when exposed to a hot surface or flame.
Thermal Oil Heater Temperature Control
The main operating parameter of a thermal oil heater is temperature. System pressure is still important for verifying pump performance and detecting abnormal resistance, but pressure alone does not determine the process temperature.
The temperature-control sequence generally operates as follows:
- The circulation pump starts.
- The system confirms adequate oil flow.
- The burner begins its purge and ignition sequence.
- The thermal-oil temperature rises toward the set point.
- The controller reduces burner firing as the temperature approaches the set point.
- The burner stops or moves to minimum firing when the upper control limit is reached.
- The circulation pump continues operating.
- When the temperature falls, the burner restarts or increases its firing rate.
- A separate high-high temperature limiter shuts the burner down if the normal controller fails.
For better temperature stability and energy efficiency, a modulating burner is recommended for processes with varying heat demand.
Essential Safety Interlocks
A properly designed thermal oil heater should consider the following safety interlocks:
- Flame failure
- Ignition failure
- Low thermal-oil flow
- High thermal-oil outlet temperature
- High-high thermal-oil temperature
- High flue-gas temperature
- Low expansion-tank level
- Burner air-pressure failure
- Fuel-pressure abnormality
- Circulation-pump trip
- Motor overload
- Emergency stop
- Power failure
- Process-flow failure, where applicable
The burner must not be permitted to operate if any critical safety condition is not satisfied.
Safe Start-Up Procedure
A typical start-up procedure includes:
- Inspect the thermal-oil level.
- Confirm that all valves are in the correct position.
- Check the expansion and collecting tanks.
- Inspect the pump, seal, coupling, and electrical supply.
- Start the circulation pump.
- Confirm adequate oil flow or differential pressure.
- Release trapped air from the system according to procedure.
- Start the burner at low firing rate.
- Increase the temperature gradually.
- Monitor pressure, temperature, flow, oil level, burner flame, and exhaust-gas temperature.
- Record operating data in the log sheet.
A new system or recently refilled system must be heated slowly to remove moisture and trapped air safely.
Safe Shutdown Procedure
During a normal shutdown:
- Stop the burner.
- Keep the circulation pump operating.
- Allow thermal oil to continue transferring residual heat.
- Continue circulation until the heater temperature falls below the manufacturer’s specified safe shutdown temperature.
- Stop the circulation pump only after the heater has cooled sufficiently.
- Record abnormal conditions found during shutdown.
Stopping the circulation pump immediately after stopping a hot burner can cause residual heat to overheat the stationary oil inside the coil.
Preventive Maintenance
Preventive maintenance should cover:
- Burner combustion adjustment
- Flame-detector inspection
- Fuel-valve tightness
- Ignition-electrode condition
- Pump vibration and alignment
- Mechanical-seal leakage
- Strainer cleanliness
- Coil inspection
- Thermal-insulation condition
- Expansion-tank level
- Thermal-oil laboratory analysis
- Safety-interlock testing
- Temperature-sensor calibration
- Pressure and flow instrument calibration
- Electrical-panel inspection
- Chimney and flue-gas inspection
Maintenance frequency should follow equipment condition, operating hours, fuel type, manufacturer recommendations, and applicable safety requirements.
Thermal Oil Heater Applications
Thermal oil heaters are widely used for:
- Chemical reactors
- Mixing tanks
- Oil and fuel storage tanks
- Rotary dryers
- Industrial ovens
- Textile machinery
- Plywood and wood-processing plants
- Asphalt mixing plants
- Food-processing equipment
- Palm-oil processing
- Rubber and plastic industries
- Marine and refinery processes
- Printing and coating machines
- Heat exchangers
- Hot presses
Each application requires a separate heat-load calculation. Heater capacity should not be selected only from the size of the production machine.
Why Choose PT Indira Mitra Boiler?
PT Indira Mitra Boiler provides thermal oil heater solutions based on process requirements, operating temperature, thermal-fluid flow, fuel availability, site conditions, and applicable safety requirements.
Our services can include:
- Thermal-load calculation
- Vertical or horizontal heater design
- Burner selection
- Heating-coil fabrication
- Circulation-pump selection
- Expansion and collecting tank design
- Control-panel assembly
- Piping and valve installation
- Instrumentation and safety interlocks
- Installation and commissioning
- Combustion tuning
- Operator training
- Maintenance and spare-parts support
Conclusion
A Thermal Oil Heater is an efficient solution for industrial processes requiring high and stable temperatures without the high operating pressure associated with steam systems.
Its performance and safety depend on correct heater design, adequate oil circulation, suitable thermal-fluid selection, reliable burner control, properly designed expansion capacity, and complete safety interlocks.
The burner must never operate without confirmed thermal-oil circulation. High-temperature, low-flow, flame-failure, expansion-tank level, and exhaust-temperature protection must be tested and maintained according to approved procedures.
For thermal oil heater design, supply, installation, commissioning, maintenance, and burner services, contact:
PT Indira Mitra Boiler
Workshop: Tangerang, Indonesia
WhatsApp: +62 813-8866-6204
Website: www.indiramitraboiler.co.id
Website: www.burner.co.id
YouTube: @BejoBurnerIndonesia
Frequently Asked Questions
What is a thermal oil heater?
A thermal oil heater is an industrial heating machine that heats thermal fluid inside a coil and circulates it to production equipment requiring controlled process heat.
What is the maximum operating temperature?
Many thermal oil systems operate at temperatures up to approximately 300–320°C. The permitted temperature depends on the thermal-fluid specification and heater design.
Does a thermal oil heater operate at high pressure?
It normally operates at lower pressure than a steam system producing a comparable temperature. Its pressure is mainly generated by the circulation pump and piping resistance.
Does thermal oil require treatment?
It does not require conventional boiler-water treatment, but the oil must be sampled and tested periodically for oxidation, contamination, viscosity changes, acidity, and thermal degradation.
Why must the circulation pump remain on after burner shutdown?
The pump removes residual heat from the heating coil. Stopping circulation while the heater is still hot may cause local overheating and thermal-oil degradation.
What happens if thermal-oil flow becomes too low?
The safety interlock must stop the burner. Insufficient flow can overheat the coil and cause oil cracking, carbon deposits, coil damage, fire, or leakage.
Which fuels can be used?
Depending on burner and heater design, the system can use natural gas, CNG, LPG, biogas, diesel, heavy fuel oil, prepared waste oil, or a dual-fuel combination.
How long does thermal oil last?
Thermal oil may remain usable for several years in a properly designed system. Its replacement interval should be based on laboratory analysis and operating condition rather than age alone.